Case Study: Retrofitting a Standard Screw Cap Mold for Tethered Closure Production
Case Study: Retrofitting a Standard Screw Cap Mold for Tethered Closure Production
Published by BOXIANG — Technical Case Study & Tooling Retrofit Guide
Executive Summary & Background
With the implementation of the European Union Single-Use Plastics (SUP) Directive (Directive EU 2019/904) and European Standard EN 17665:2022, global beverage brand owners and packaging converters faced an urgent operational mandate: convert all existing detachable closure lines to tethered caps. Purchasing completely new high-cavitation tooling systems requires significant capital expenditure (CAPEX) and extended equipment delivery lead times.
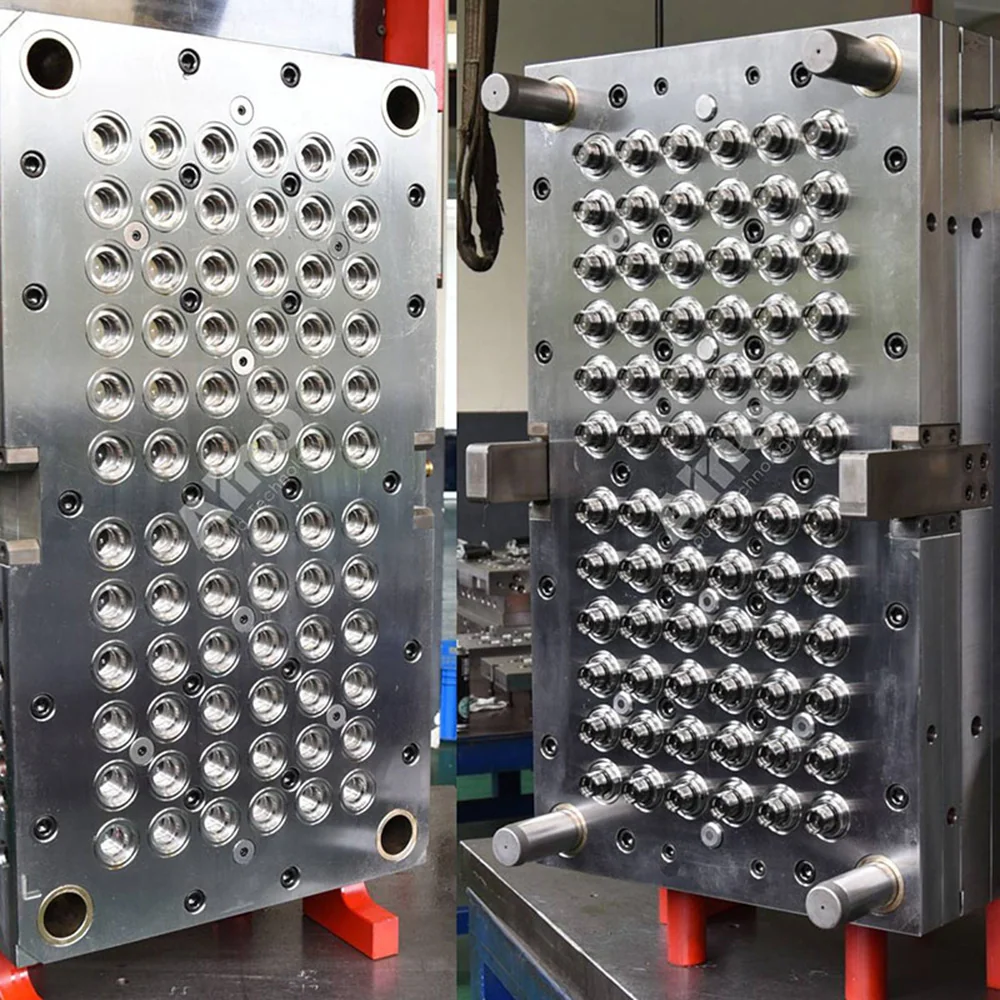
To mitigate costs and accelerate compliance timelines, a leading international beverage packaging converter partnered with BOXIANG to evaluate and execute a complete tooling retrofit. This case study details how our engineering team modified a high-cavitation standard 38mm screw cap mold into a fully compliant tethered closure tool, preserving over 70% of original mold base assets while maintaining rapid cycle efficiency.
1. Initial Audit and Technical Feasibility Assessment
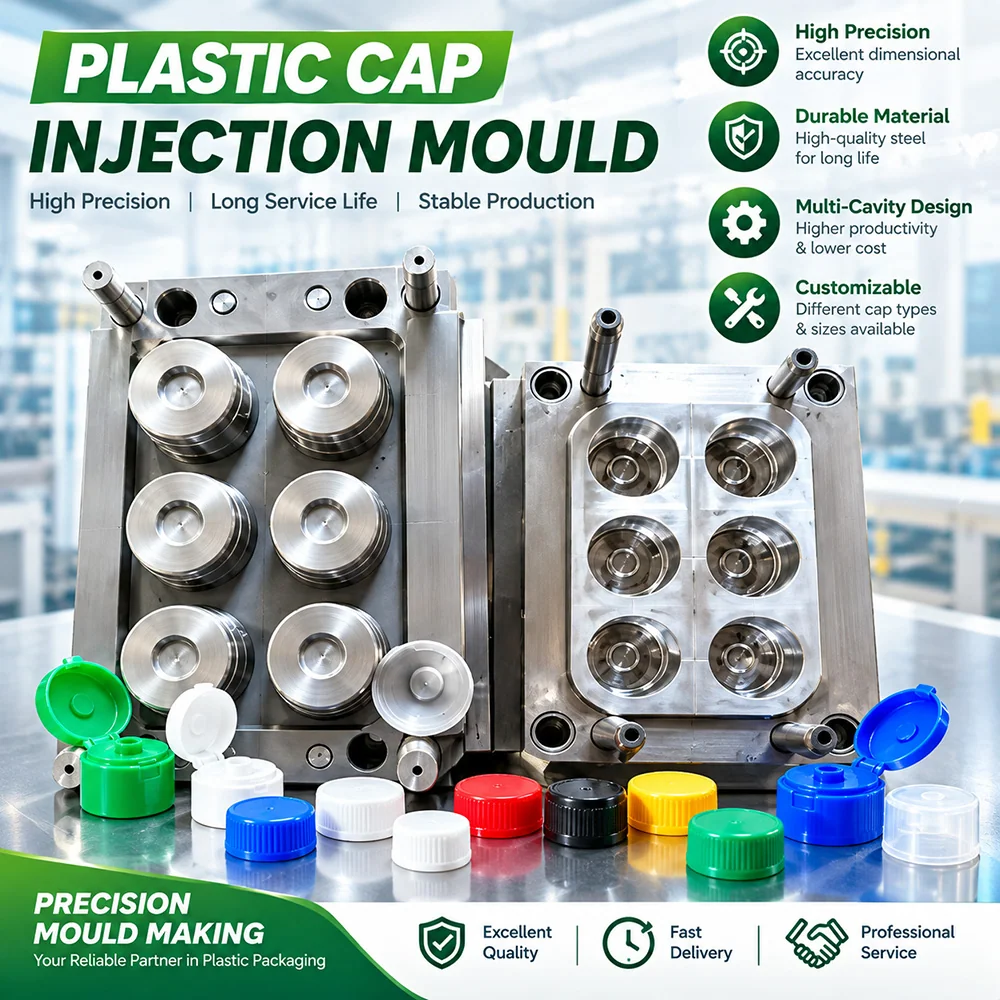
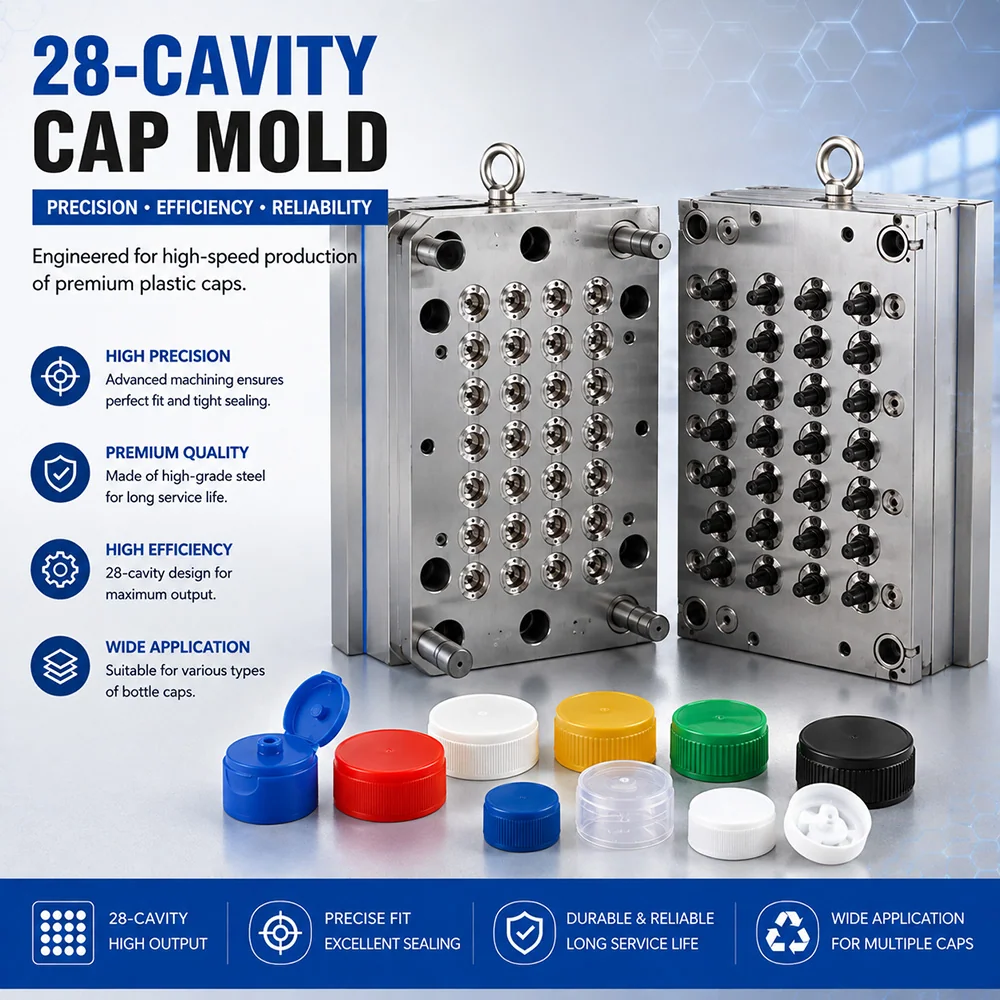
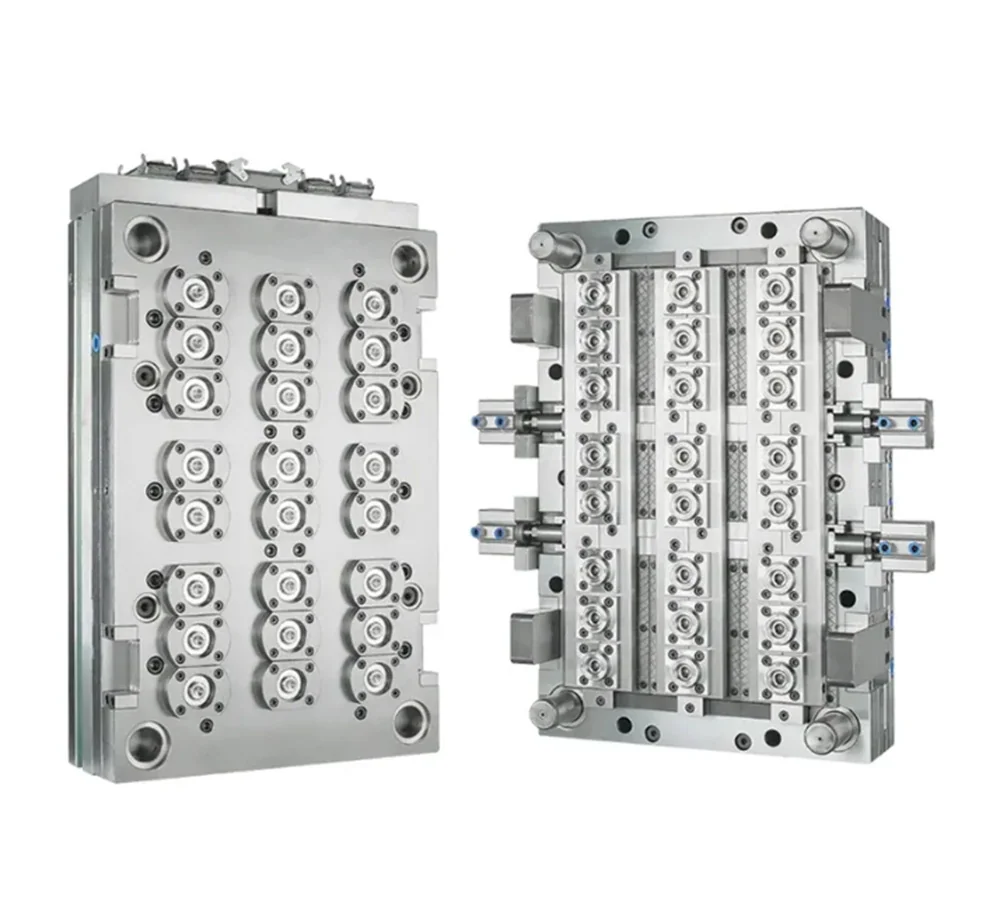
Retrofitting a standard cap mold for tethered compliance requires more than swapping cavity inserts. The existing tool—a 32-cavity unscrewing and stripping combination mold—was evaluated across key engineering parameters to ensure structural compatibility with tethered geometries.
Key Evaluation Parameters:
- Neck Finish Geometry & Thread Engagement: Verifying that modified closure features preserve sealing integrity on existing PET bottle neck finishes (e.g., 1881 / 29/25 standards) without increasing capping torque.
- Ejection Stroke and Daylight Clearance: Assessing whether additional mechanical lifters or modified stripper plates required extra machine opening stroke on existing injection molding machines (IMMs).
- Hot Runner Manifold Pitch & Gate Layout: Ensuring existing nozzle positions aligned with modified cavity core pin centerlines.
2. Tooling Retrofit Engineering: Modified Core Inserts and Slitting Integration
To convert the detachable tamper-evident (TE) band into a functional tether strap capable of withstanding >25 N pull force, BOXIANG implemented a hybrid engineering solution combining modified cavity inserts and downstream high-speed slitting integration.
| Retrofit Component | Legacy Tooling Setup | BOXIANG Re-Engineered Solution | Engineering Result |
|---|---|---|---|
| Cavity Insert | Standard smooth neck ring with continuous TE band groove | Precision-milled retaining band cavity with tether hinge geometry | Forms integrated tether joints directly in the mold without flashing |
| Core Pin Insert | Standard straight cooling channel core | 3D printed conformal cooling core insert with optimized BeCu tip | Absorbs extra thermal load around tether bridges; prevents sink marks |
| Ejection Assembly | Single-stage mechanical stripper plate | Two-stage controlled stripping plate with guided core retention pins | Ejects complex tether band without stretching or tearing retaining bridges |
3. Thermal Optimization and Cycle Time Preservation
Adding tethered hinge features often increases local wall thickness variations, threatening to extend cooling time and reduce hourly output. BOXIANG solved this bottleneck through advanced metallurgical and thermal engineering.
- Conformal Cooling Retrofit: We replaced original solid core pins with direct-metal laser sintered (DMLS) 1.2344 steel cores featuring conformal fluid channels, cooling the hinge web area up to 30% faster.
- Beryllium Copper (BeCu) Core Tips: High thermal conductivity BeCu inserts were press-fitted into deep thread zones to rapidly pull heat away from internal sealing lips.
- Cycle Time Outcome: The retrofitted 32-cavity tool achieved a steady production cycle time of 5.8 seconds, fully matching the legacy tool's baseline output speed.
4. Quality Validation, EN 17665 Testing, and Production ROI
Following in-house trial runs at our manufacturing facility in China, samples from all 32 cavities underwent rigorous Quality Assurance testing to verify compliance and structural integrity.
Validation Results:
- Tensile Pull Resistance: Tether straps demonstrated mechanical resistance to tensile loads exceeding 32 N (surpassing the mandatory 25 N EN 17665 threshold).
- Ergonomic Opening Angle: Integrated hinge mechanisms maintained closure park positions at >135 degrees, providing unobstructed pouring and drinking access.
- CAPEX & Lead Time Savings: Retrofitting the existing mold base reduced total project capital investment by 62% compared to purchasing a new tool, while cutting project delivery lead time from 16 weeks to 6 weeks.
Partner with BOXIANG for Precision Closure Tooling & Retrofit Services
At BOXIANG, we provide comprehensive, end-to-end plastic cap mold solutions—from initial DFM and prototype development to high-cavitation tooling production and legacy mold retrofits. Our specialized focus on closure mold engineering guarantees fast cycle times, sub-micron component interchangeability, and full compliance with global regulatory standards.
Whether you need new high-speed tethered cap molds or seek to modernize existing tooling assets, BOXIANG delivers the technical expertise and manufacturing precision required to keep your production lines profitable and compliant.